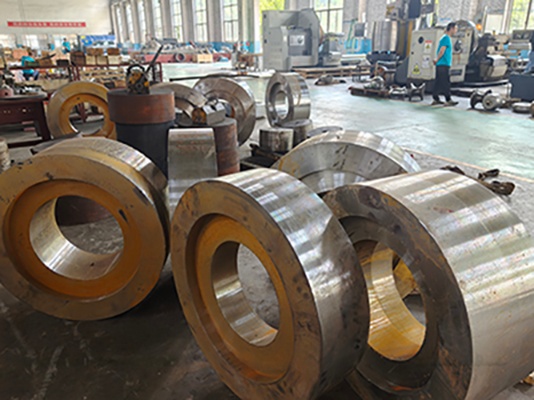
Stainless steel welded tube roll forming relies on progressive roll sets to gradually bend flat stainless strip into a circular profile before welding. Unlike carbon steel, stainless materials feature obvious work hardening, significant springback and high risk of surface scratching. Improper roll selection will lead to strip edge cracking, tube ovality, surface galling, unstable weld seam and frequent roll wear. Selecting matched forming rolls requires comprehensive consideration of tube specifications, stainless steel grades, forming process, roll material, pass profile and surface treatment. This article sorts out core selection principles to support stable stainless steel tube production.
1. Understand Material Characteristics of Stainless Steel as the Precondition
Common stainless grades including 304, 316L, duplex stainless steel have distinct forming properties, which determine roll design and configuration.
Austenitic stainless steel (304 / 316L): high work hardening rate, large springback. Each forming pass must adopt small incremental deformation to avoid edge cracks. Roll pass curve needs reserved springback compensation.
Duplex stainless steel: higher yield strength, demanding uniform pressure distribution; excessive local compression easily triggers material fracture.
Thin-wall stainless strip: sensitive to scratch. Rolls must achieve ultra-smooth surface and uniform contact to eliminate linear marks.
When configuring roll stands, the deformation amount of each pass should be controlled reasonably. Avoid sharp bending radii that concentrate stress on the strip edge.
2. Select Roll Base Material and Hardness According to Production Load
Roll substrate directly affects wear resistance, toughness and service life, which is a core selection index.
Common roll materials for stainless tube forming
Cr12MoV / SKD11 (D2)The most widely used general-grade tool steel. After vacuum heat treatment, hardness reaches HRC 58–62. It balances wear resistance and impact toughness, suitable for conventional 304 / 316L tube mass production with medium line speed. It works for both thin-wall and medium-wall stainless tubes.
High-speed steel (M2)Higher thermal stability and wear resistance than Cr12MoV. Ideal for high-speed forming lines, thick-wall stainless tubes or duplex stainless steel production where roll bears heavy continuous load.
Cemented carbideExtreme wear resistance, used for high-precision bright stainless tube, high-volume continuous production. Higher manufacturing cost, mainly applied to sizing rolls and fin passes with high friction.
Selection reference:
Small batch, low-speed production of decorative stainless tubes: Cr12MoV is cost-effective;
High-speed continuous production, industrial fluid stainless tubes: adopt high-speed steel or carbide rolls;
Avoid over-high hardness without matching toughness. Excessively hard rolls are prone to edge chipping under impact load.
3. Optimize Pass Profile & Progressive Flower Design
Pass profile determines the deformation path of stainless strip and directly restrains forming defects.
Progressive bending principleThe strip is bent step by step through breakdown passes, fin passes and sizing passes. Do not pursue one-step large deformation. The roll flower design must disperse bending strain and prevent edge wave, edge cracking.
Pass curve typeInvolute or multi-curve pass is preferred for stainless forming. It realizes uniform contact between roll and strip, reduces relative sliding, and lowers surface scratch risk. Simple circular arc passes easily cause local sliding and galling.
Roll gap matchingSet reserved gap according to strip thickness. Too small gap squeezes the strip and causes work hardening; excessive gap leads to insufficient forming and poor roundness. For thin-wall stainless strips, roll gap control accuracy should reach ±0.02 mm.
Fin pass special requirementsFin rolls control the V-shape opening before welding. The gap between strip edges affects welding stability. Rolls must keep symmetrical to prevent strip edge misalignment.
4. Surface Treatment of Rolls to Prevent Stainless Scratching & Galling
Stainless steel tends to produce adhesion friction when sliding against metal rolls. Surface coating is essential for surface quality control of finished tubes.Available surface solutions:
Precision superfinishingRa ≤ 0.2 μm base surface, removes tool marks, reduces metal adhesion risk. It is the basic requirement for bright stainless tube production.
Hard chrome platingImproves surface hardness and smoothness, suitable for general decorative stainless tubes. Attention should be paid to coating thickness to avoid peeling under heavy load.
PVD coating (TiN, TiCN)Low friction coefficient, excellent anti-galling performance. The preferred option for high-standard industrial stainless tubes and thin-wall bright tubes, effectively suppressing surface pull marks.
Tip: Avoid using uncoated rough machined rolls to process surface-finished stainless strips. Direct metal contact will cause irreversible scratches.
5. Match Roll Configuration with Forming Line Layout
Roll sets are divided into horizontal rolls, vertical rolls, guide rolls, fin rolls and sizing rolls. Different positions bear different loads, so differentiated configuration is required.
Breakdown horizontal rolls: bear large bending force; prioritize toughness and uniform hardness;
Vertical side rolls: mainly control strip centering, prevent lateral deviation; surface smoothness must be guaranteed;
Fin rolls and sizing rolls: high frequency of friction contact; adopt higher-grade material and advanced coating;
Guide rolls: focus on surface finish to avoid scratch on strip surface.
Confirm roll inner hole tolerance, concentricity and runout. Total indicator runout (TIR) controlled below 0.03 mm ensures stable operation and uniform pressure during high-speed forming.
6. Balance Versatile Rolls and Dedicated Single-Specification Rolls
Two mainstream roll schemes for production lines:
Dedicated rolls for single tube ODPass curve fully optimized for fixed outer diameter and wall thickness. Forming stability is better, tube roundness tolerance is tighter, recommended for mass single-spec production.
Shared universal roll setsSuitable for factories producing multiple tube sizes with frequent size changeover. But the deformation compatibility is limited. Not recommended for thin-wall bright stainless tubes with strict surface requirements.
Manufacturers should evaluate order mix. Frequent size switching can adopt modular shared rolls; long-run fixed specifications deploy dedicated forming rolls.
7. Practical Selection Avoidance & Defect Prevention
Common mistakes in roll selection for stainless tube forming:
Copy carbon steel roll design directly. Ignoring stainless springback and work hardening leads to cracks and poor roundness;
Only focus on hardness without surface treatment, resulting in continuous tube surface scratches;
Excessively simplified pass stations, overloading deformation of each stand;
Low precision rough rolls for bright stainless tube production, raising scrap rate.
After roll commissioning, track tube ovality, surface quality and roll wear speed. Adjust pass profile or surface coating if early wear or galling occurs.
Conclusion
Selecting proper rolls for stainless steel tube forming relies on systematic matching: start from stainless grade and tube wall thickness, confirm roll base material and hardness, optimize progressive pass profile, select suitable anti-galling surface treatment, and configure differentiated rolls for each forming station.
There is no universal roll solution for all working conditions. For decorative stainless tubes, surface anti-scratch performance is the priority; for industrial thick-wall or duplex stainless tubes, roll load capacity and wear resistance become key indicators. Reasonable roll matching can effectively reduce forming defects, lower roll regrind frequency and improve the overall yield of stainless welded tubes.


Contact Person: Ms Liu
Tel: +86-17736028207
Email: mirror.liu@hongqiroll.com
Web: www.hongqiroll.com
Address: Chenglang Section, Jicun Town
Yuanshi County, Shijiazhuang City, Hebei, China, 051131
Copyright © 2025 Shijiazhuang Hongqi Roll Manufacturing Co., Ltd All rights reserved
Friendship Link Check Valve